Best Industrial Flooring Types by Industry: Choosing the Right Solution for Your Business
1 October 2026
Industrial flooring impacts the safety, efficiency and longevity of any commercial or industrial facility. Choosing the best industrial flooring can improve productivity, reduce maintenance costs and help businesses to meet industry regulations.
With so many flooring systems available, selecting the right solution isn’t always straightforward. Different industries face unique challenges, including heavy machinery, chemical exposure, moisture, high footfall and strict hygiene requirements.
Why Choosing the Best Industrial Flooring Matters
Industrial flooring forms part of your building’s infrastructure and directly impacts workplace safety, operational efficiency and maintenance requirements. The right flooring can provide:
- Excellent durability under heavy traffic
- Resistance to chemicals, oils and spills
- Improved slip resistance
- Easy cleaning and maintenance
- Reduced downtime for repairs
- Compliance with health and safety standards
- Long-term cost savings
Investing in the best industrial flooring for your environment helps to protect your employees, equipment and operations.
The Best Industrial Flooring for Your Industry
The below recommendations are generalised; for tailored advice to your space, please contact us for support and a personal flooring quote.
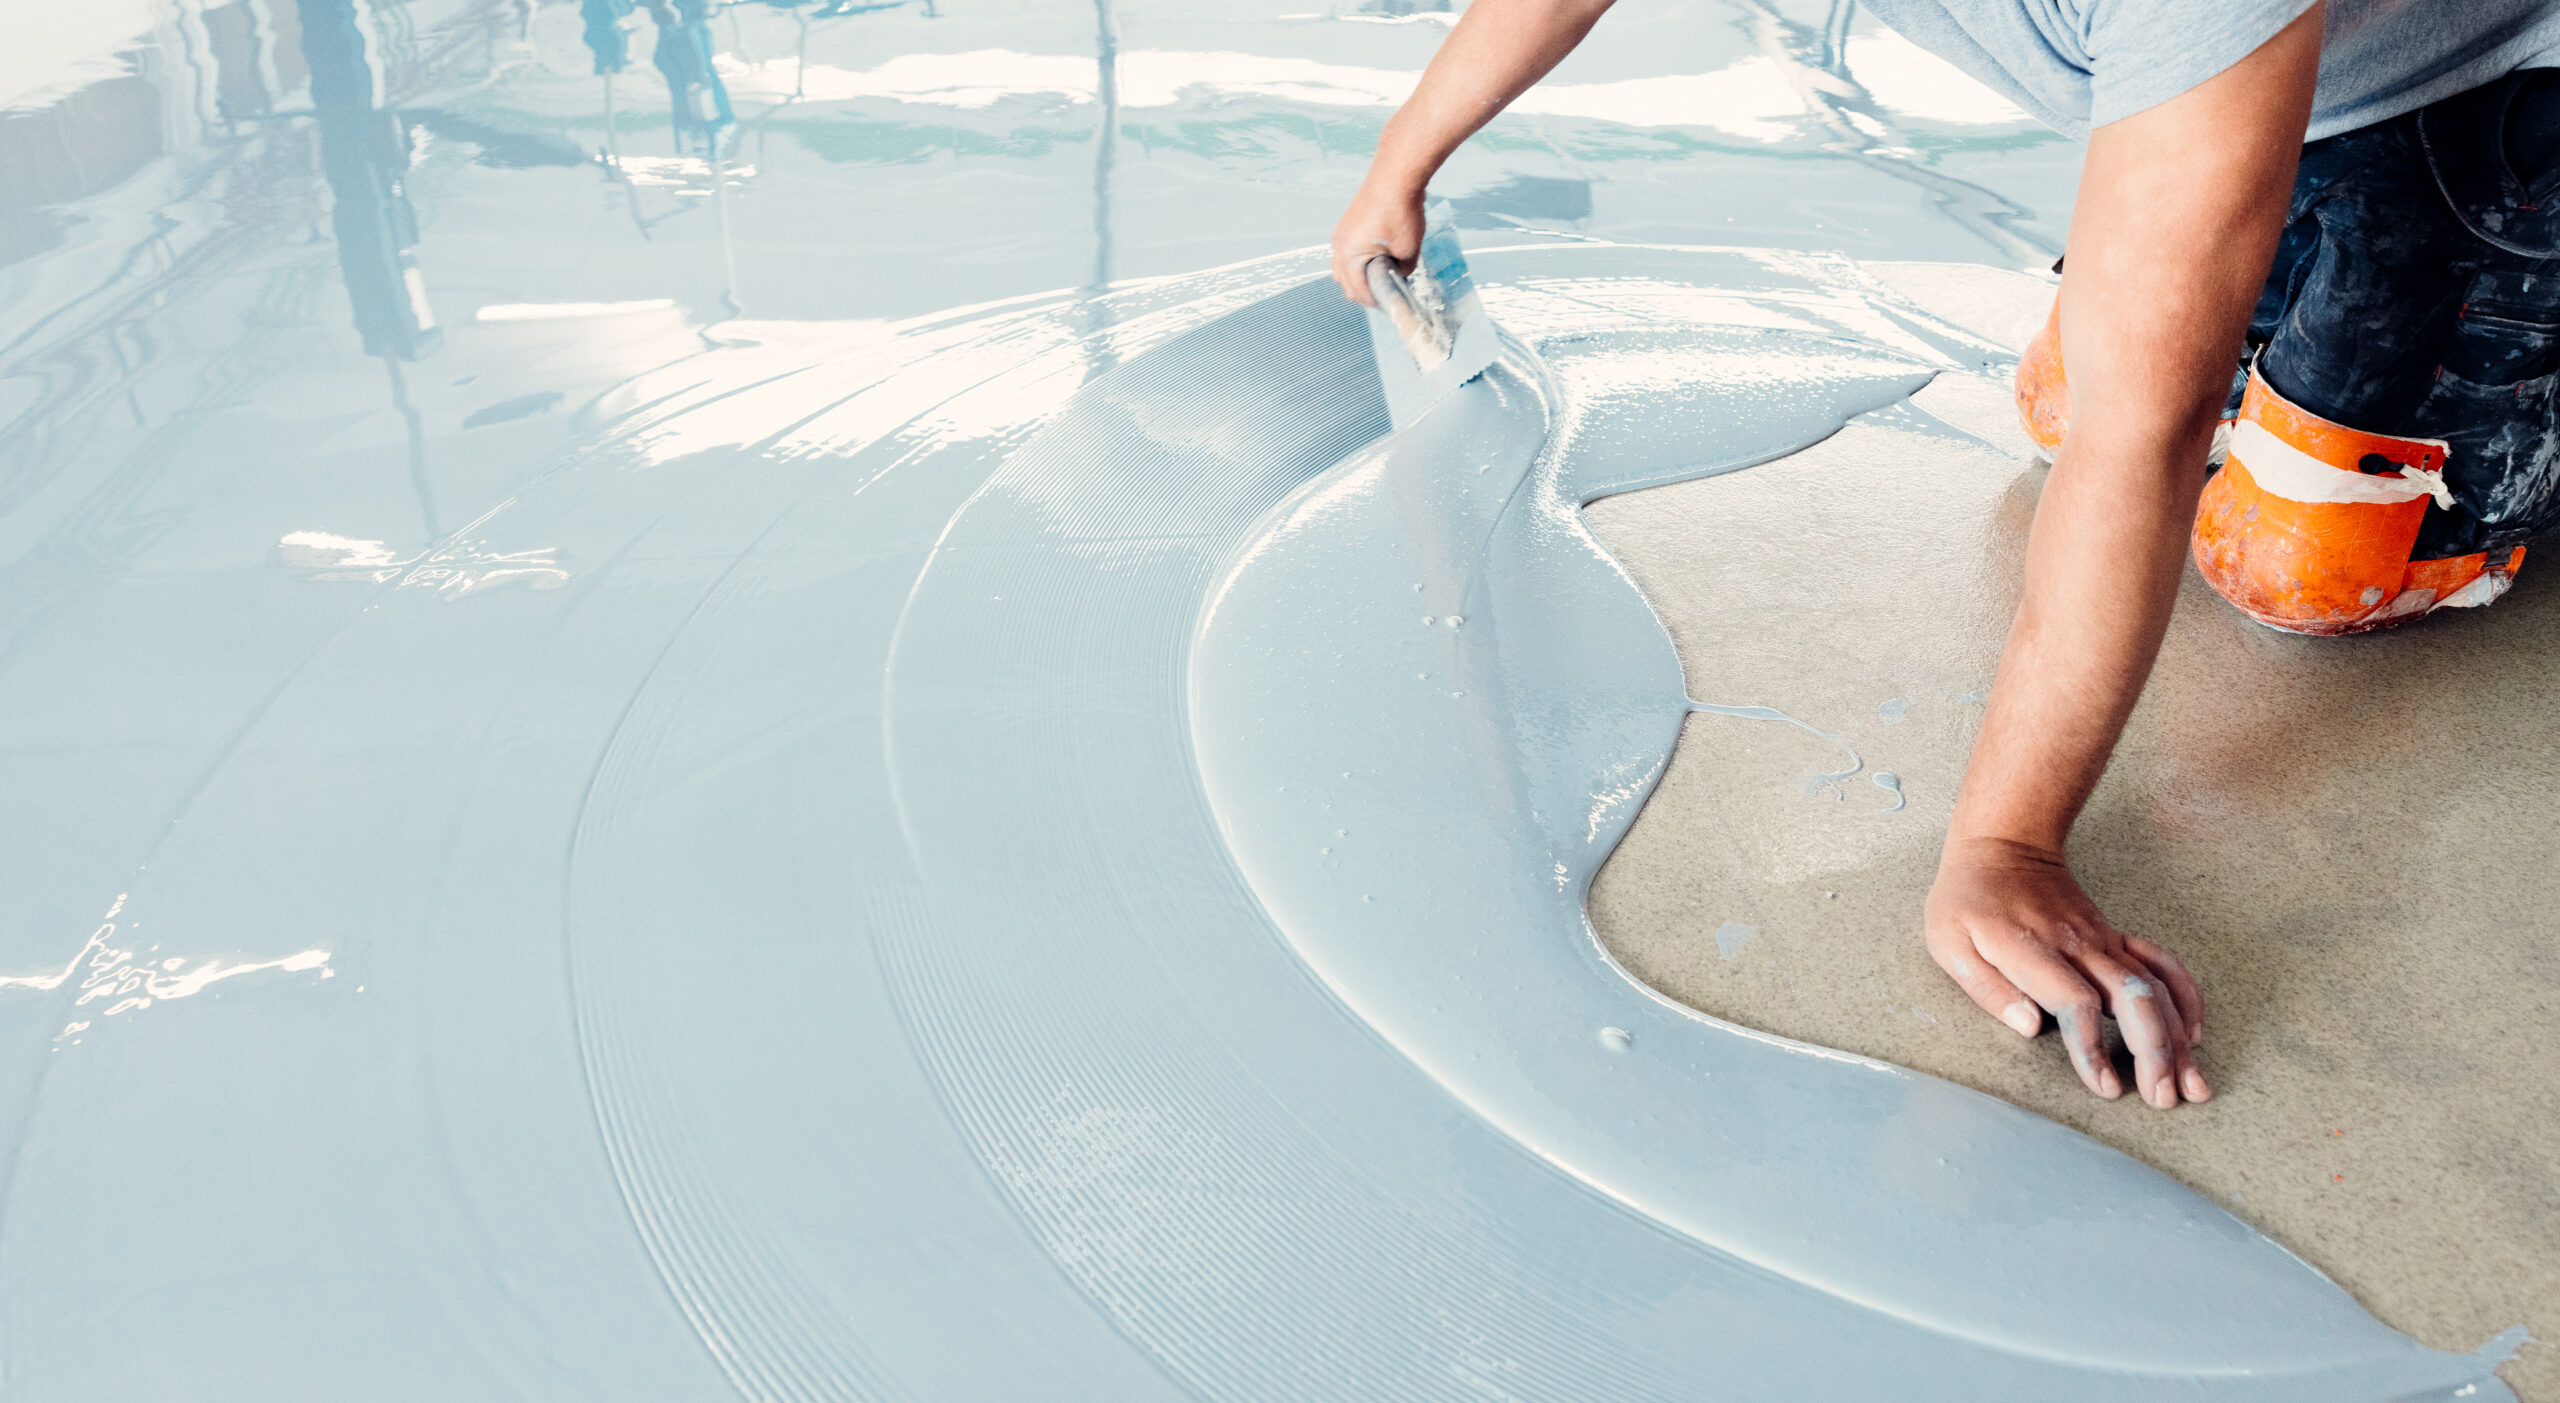
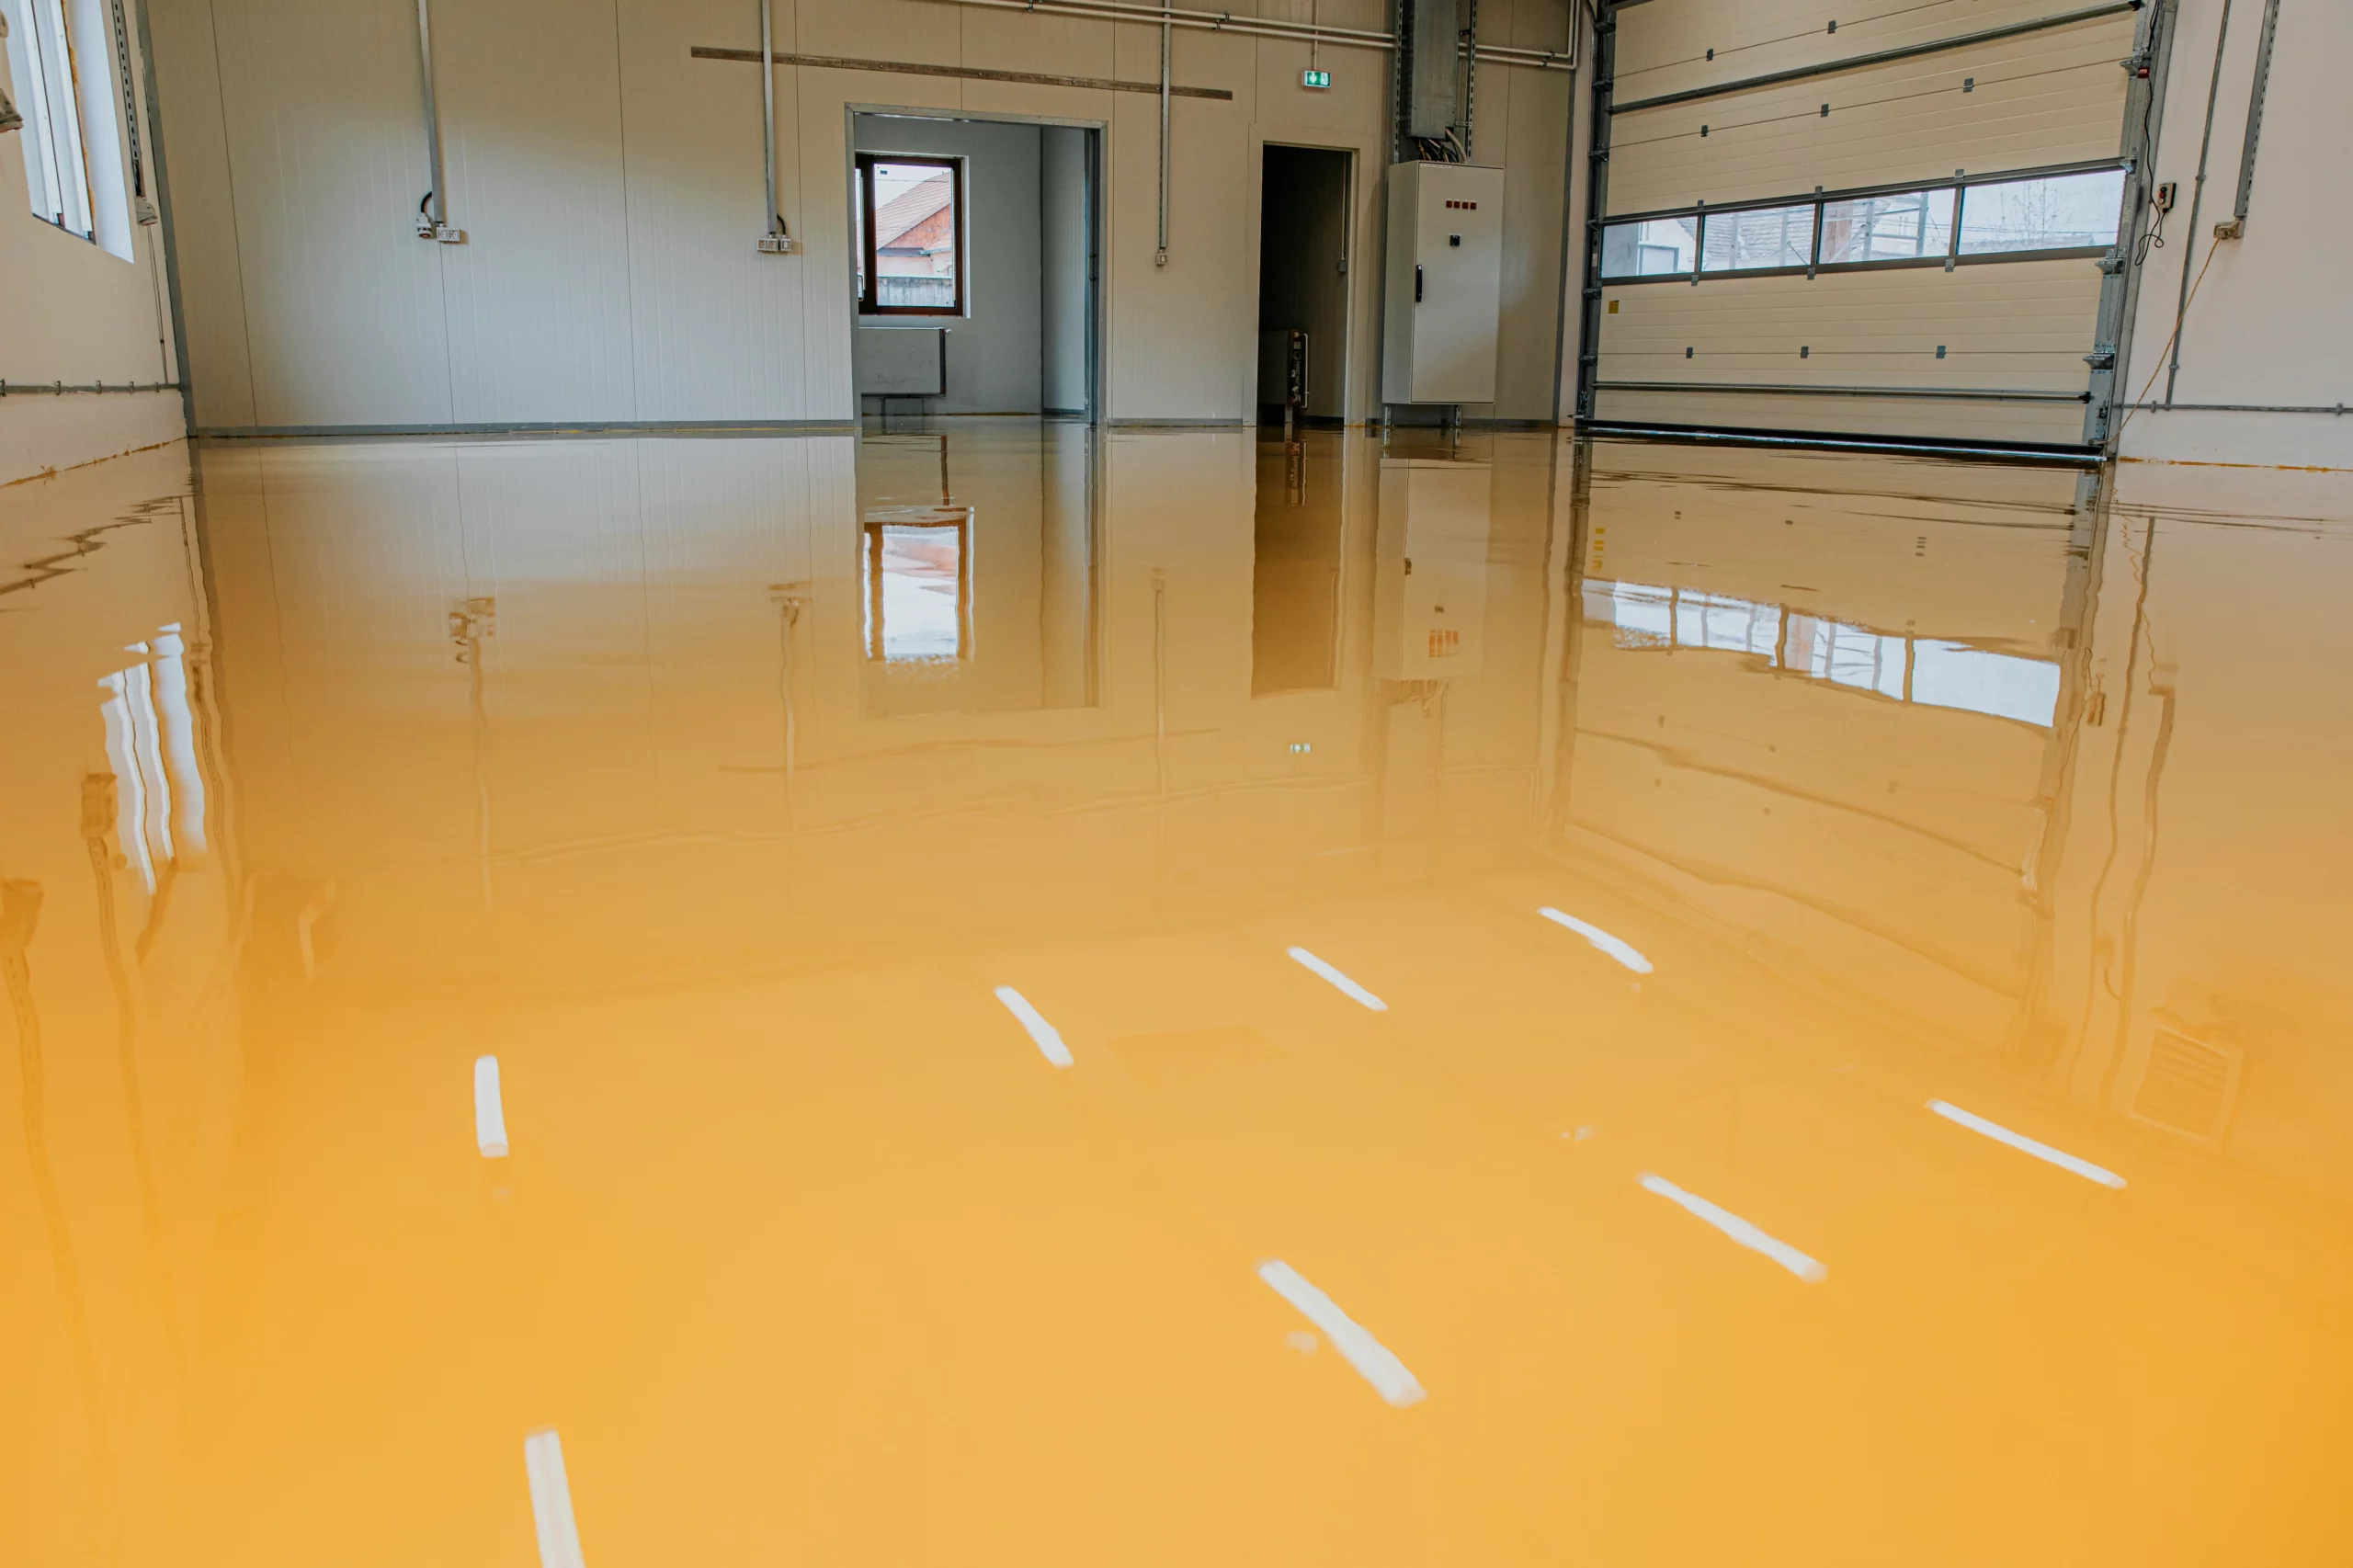
Manufacturing Facilities: Epoxy Resin Flooring
Manufacturing environments place a lot of stress on flooring. Heavy machinery, forklifts, pallet trucks and constant foot traffic demand a highly durable surface.
Epoxy resin flooring is one of the most popular industrial flooring systems for manufacturing facilities because it offers:
- High strength and durability
- Strong resistance to abrasion
- Protection against oil, grease and chemicals
- Smooth finish for easy cleaning
- Long service life
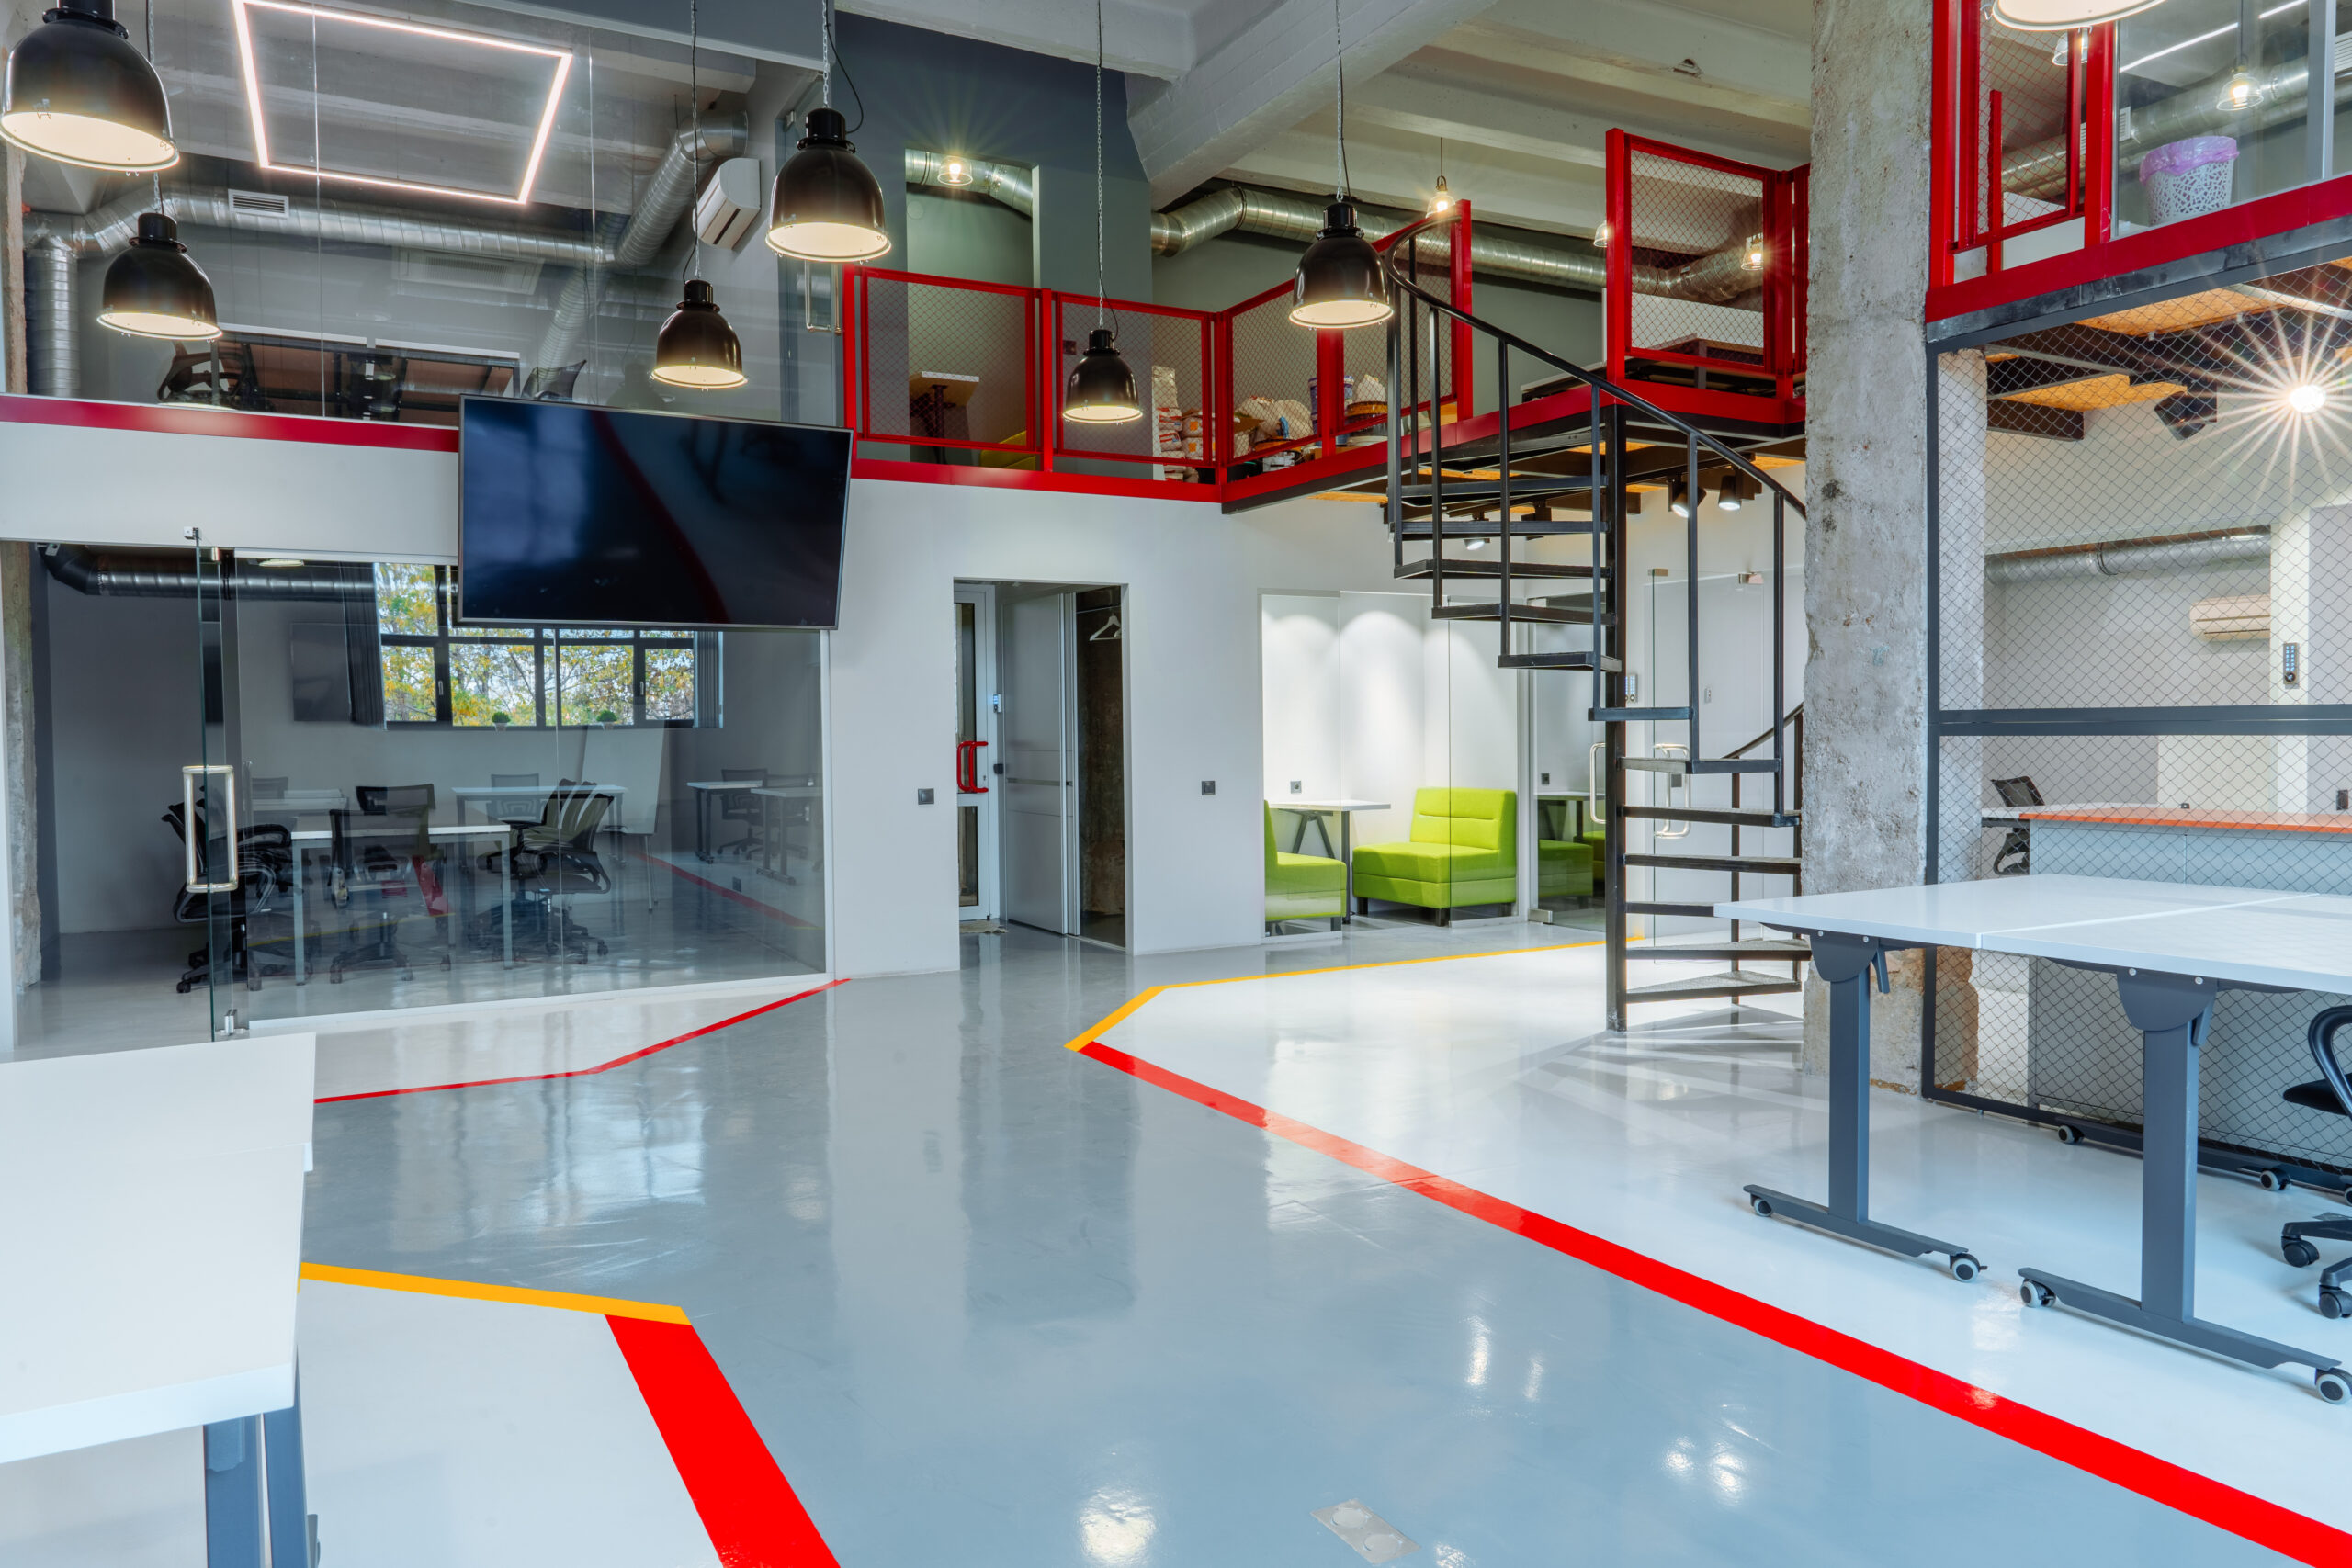
Epoxy flooring can also be customised with anti-slip finishes, line markings and colour-coded zones to improve workplace safety.
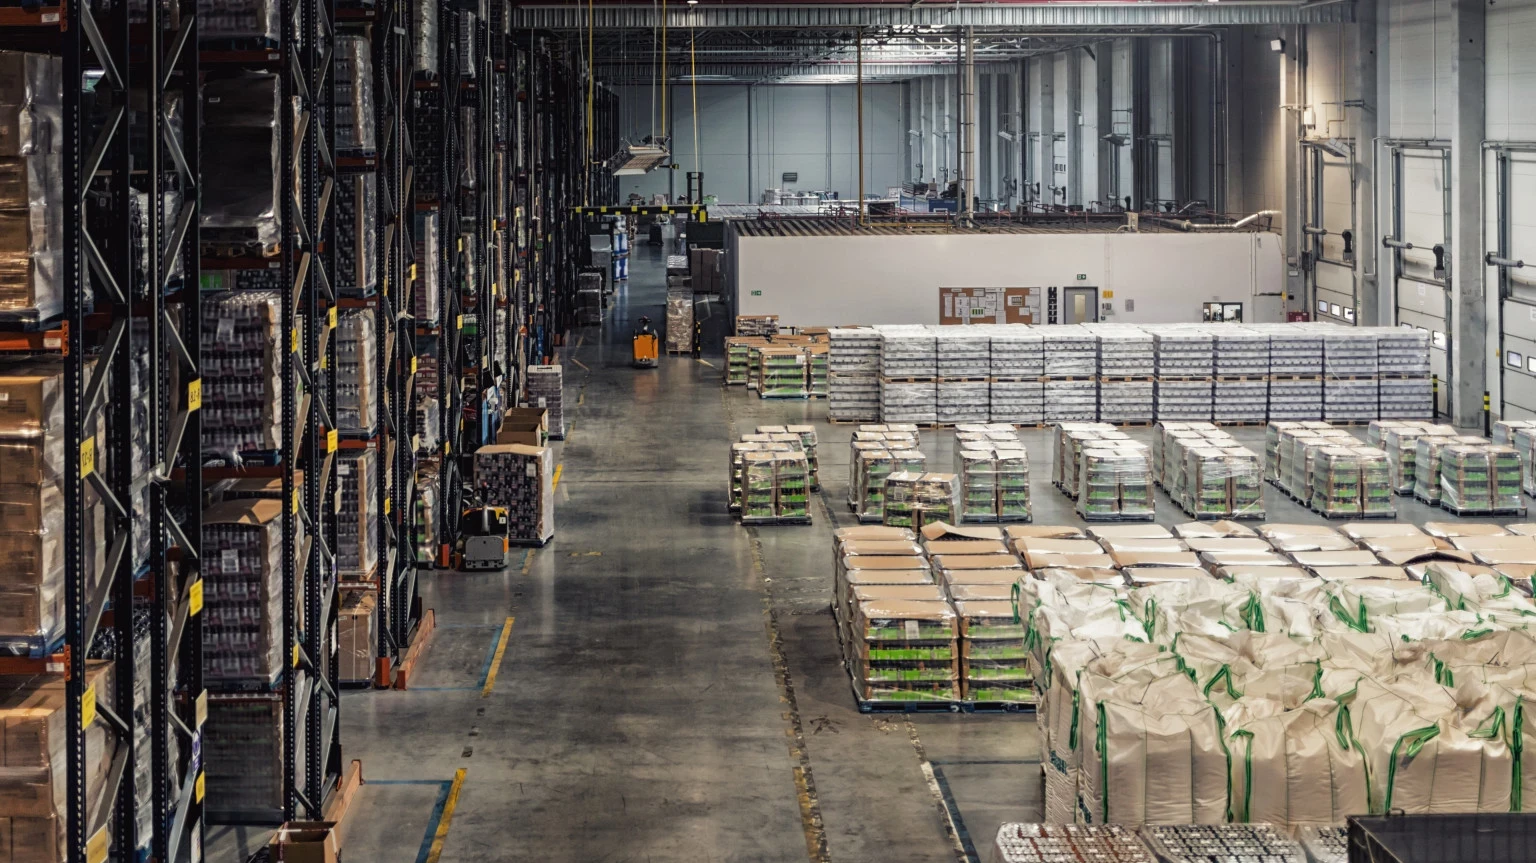
Warehouses/Distribution Centres: Heavy-Duty Resin Flooring
Warehouses experience constant movement from forklifts, loading equipment and storage systems. Flooring must withstand heavy loads without cracking or deteriorating. Heavy-duty resin flooring provides:
- High impact resistance
- Excellent load-bearing capacity
- Dust-free surface
- Easy maintenance
- Long-lasting performance
A smooth but slip-resistant finish also allows forklifts and automated vehicles to operate safely and efficiently.
Food and Beverage Facilities: Polyurethane Flooring
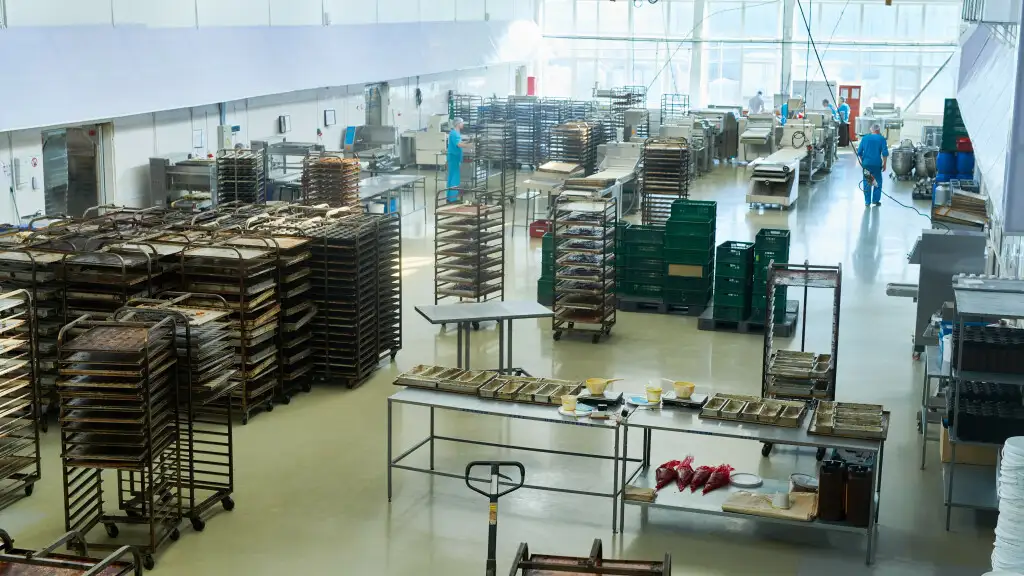
Food manufacturing and processing plants must maintain the highest hygiene standards while coping with moisture, temperature fluctuations and frequent cleaning. Polyurethane flooring is widely regarded as one of the best industrial flooring solutions for food production because it offers:
- Excellent thermal shock resistance
- High chemical resistance
- Slip-resistant finishes
- Hygienic seamless surface
- Resistance to hot water and steam cleaning
Its non-porous surface minimises bacterial growth and supports compliance with food hygiene regulations.
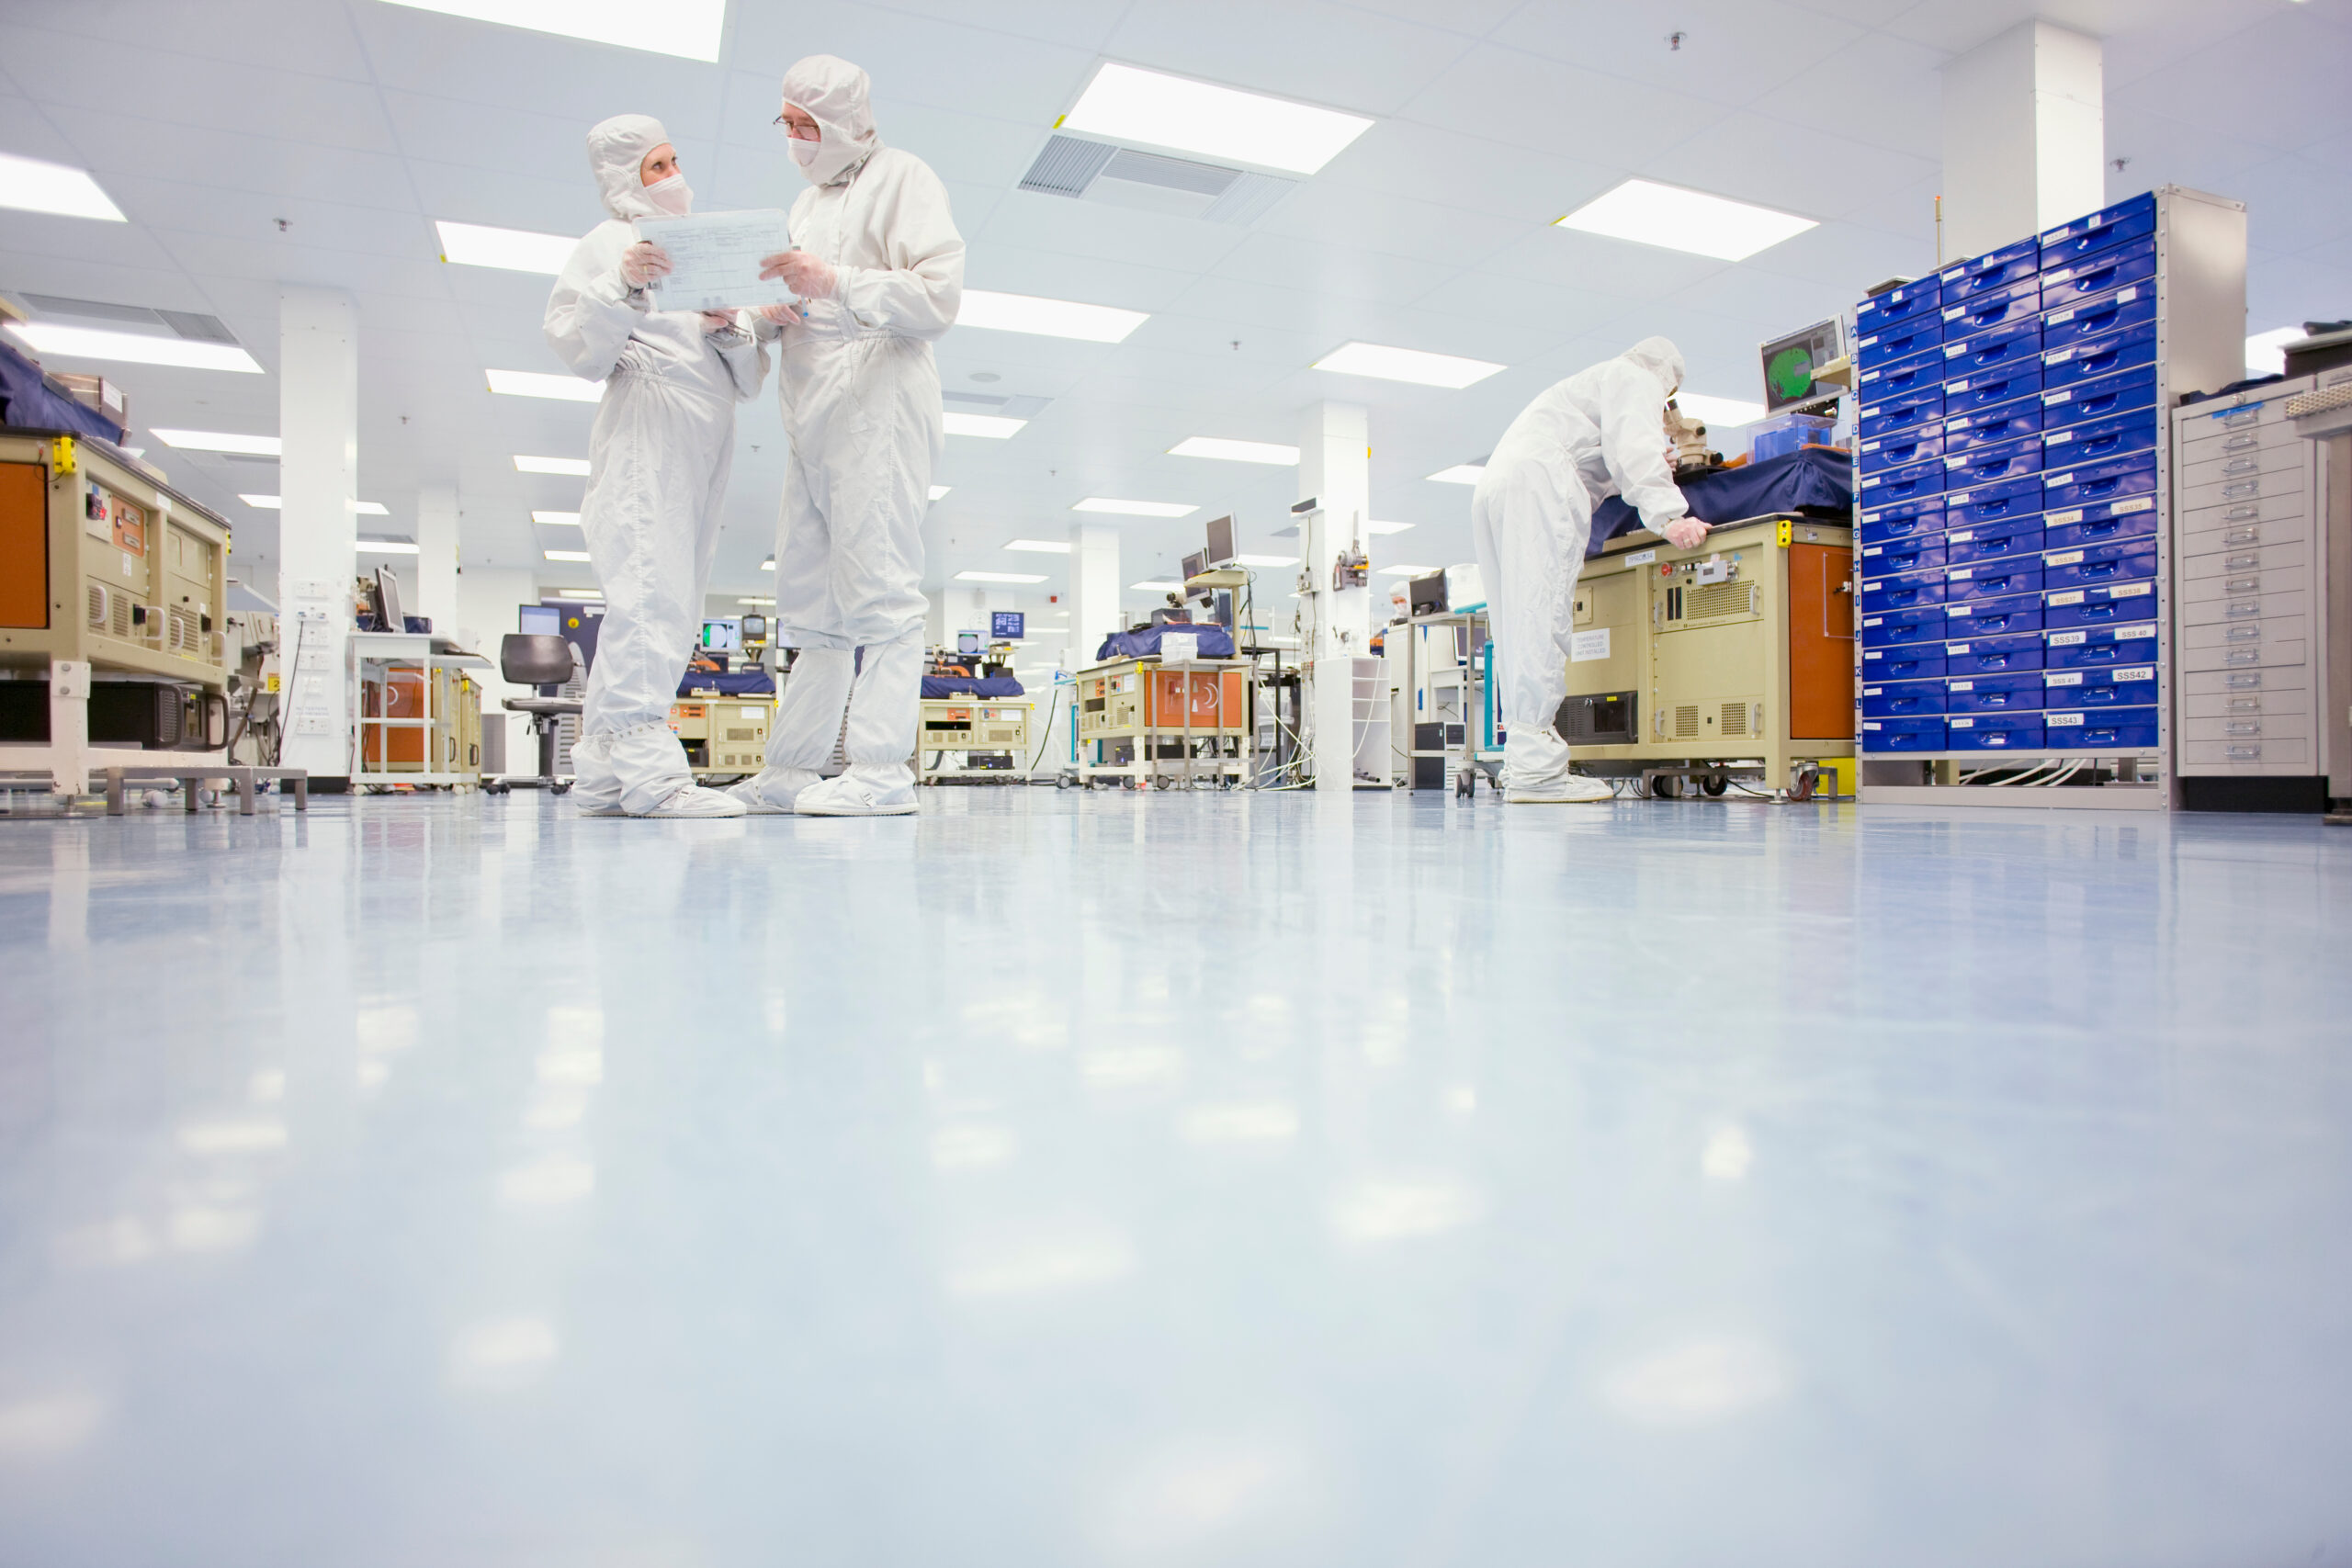
Pharmaceutical and Healthcare Facilities: Resin Flooring
Healthcare and pharmaceutical environments require flooring that supports strict infection control procedures while remaining durable and easy to clean. Seamless resin flooring provides:
- Hygienic, non-porous surfaces
- Easy cleaning and sanitisation
- Chemical resistance
- Low maintenance requirements
- Attractive appearance
Many systems also incorporate antimicrobial properties, making them ideal for sterile environments.
Automotive Workshops: Chemical-Resistant Epoxy Flooring
Vehicle workshops face exposure to oils, fuels, solvents and heavy equipment. Flooring must resist staining and chemical damage while remaining safe underfoot. Epoxy flooring is particularly well suited to automotive environments because it offers:
- Resistance to oils and fuels
- High impact resistance
- Easy cleaning after spills
- Attractive professional finish
- Excellent durability
Slip-resistant additives can further improve safety in areas where liquids are regularly present.
Engineering: Heavy-Duty Industrial Concrete with Resin Coating
Engineering facilities house large machinery, welding operations and heavy manufacturing processes that demand extremely resilient flooring. This combination provides:
- Outstanding structural strength
- Excellent wear resistance
- Protection against impact damage
- Dust reduction
- Improved surface durability
The resin coating also simplifies cleaning while extending the lifespan of the concrete beneath.
Retail and Commercial Spaces: Decorative Resin Flooring
Retail warehouses and commercial facilities require flooring that is hard-wearing with a pleasing appearance. Decorative resin flooring offers:
- Modern professional appearance
- Long-lasting finish
- Easy maintenance
- Resistance to high foot traffic
- Available in various colours and finishes
This makes it ideal for customer-facing environments where aesthetics matter alongside performance.
Factors to Consider When Choosing the Best Industrial Flooring
Every workplace has different operational requirements. Before selecting a flooring system, consider:
- Traffic Levels: Assess whether the flooring will experience pedestrian traffic, forklift movements or heavy machinery.
- Chemical Exposure: Choose flooring with suitable chemical resistance if oils, solvents or cleaning agents are regularly used.
- Hygiene Requirements: Industries such as food production and healthcare benefit from a flooring solution that is easy to sanitise.
- Slip Resistance: Safety should always be a priority. Anti-slip finishes can significantly reduce the risk of workplace accidents.
- Temperature Changes: Some industrial environments experience rapid temperature fluctuations. Polyurethane flooring systems perform particularly well under thermal stress.
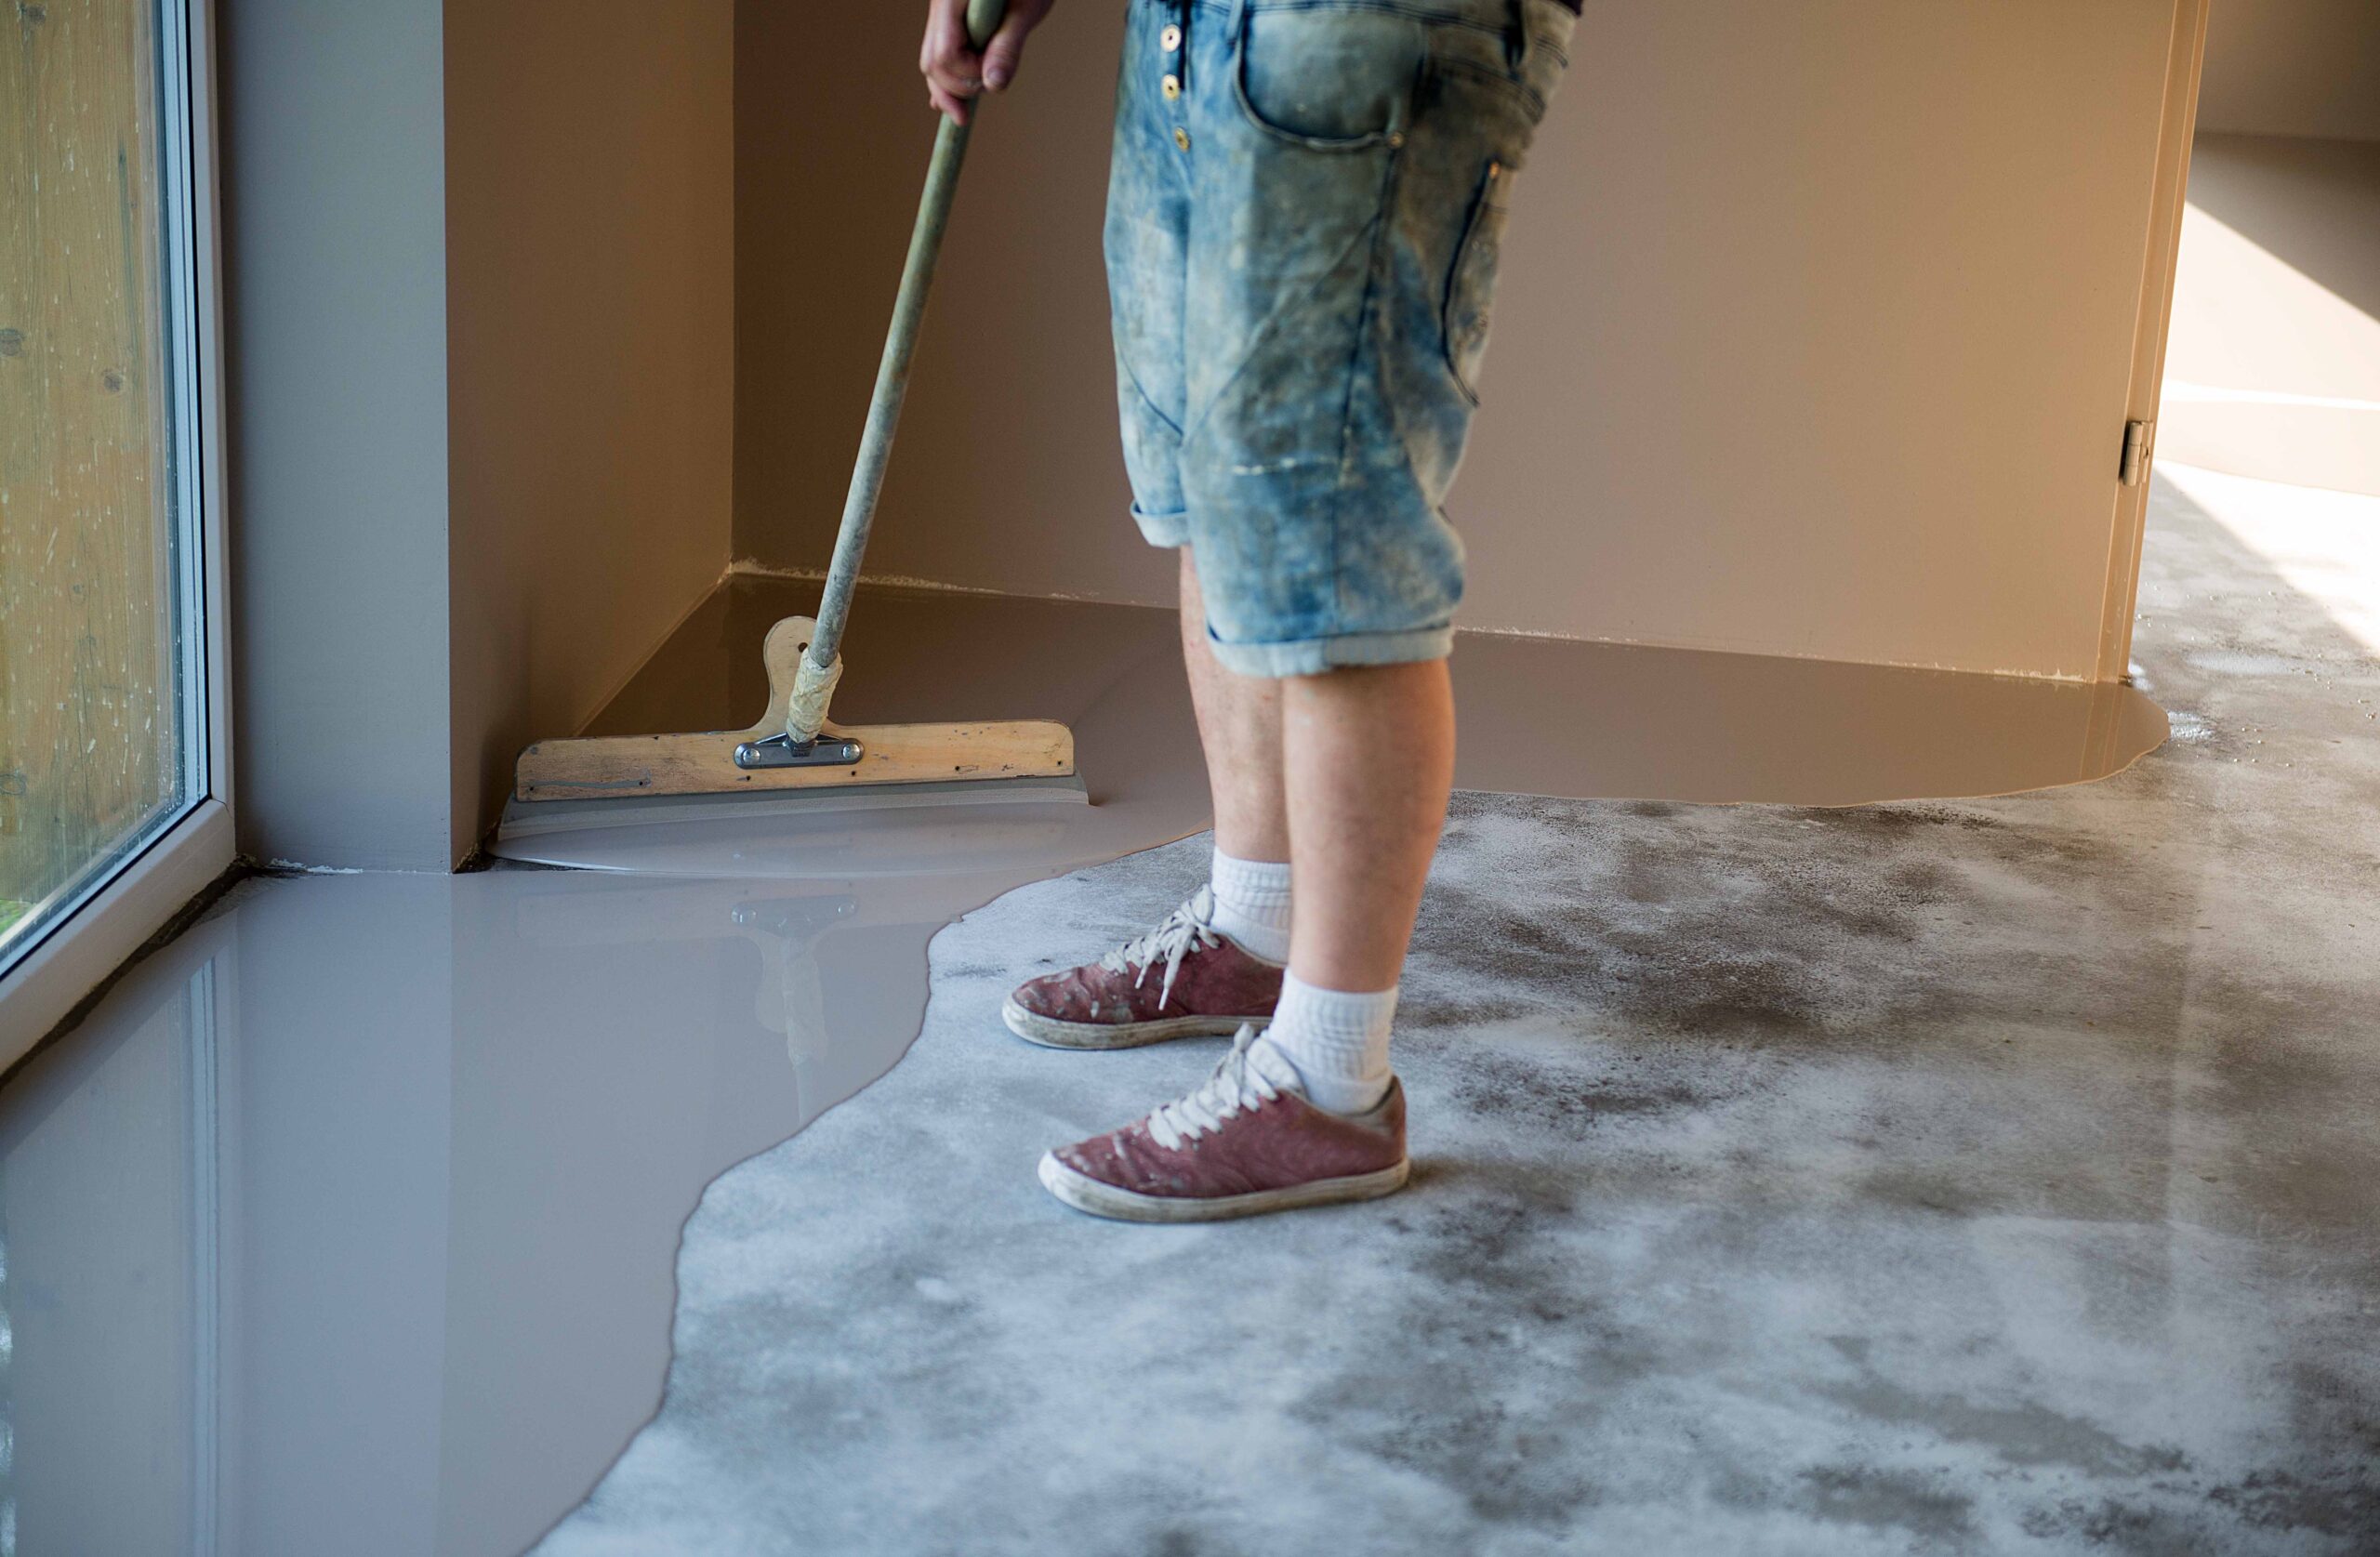
- Installation Downtime: Minimising operational disruption is often essential. Some resin flooring systems cure more quickly than others, allowing businesses to resume operations sooner.
Maintaining Industrial Flooring
Regular maintenance extends the life of your flooring and keeps facilities safe. Simple maintenance practices include:
- Routine cleaning to remove dirt and debris
- Prompt removal of chemical spills
- Regular inspections for wear or damage
- Scheduled repairs before small issues become major problems
- Professional maintenance to maximise flooring lifespan
A proactive maintenance programme reduces costly downtime and protects your flooring for years to come.
Solutions for Industrial Floors
There is no single flooring system that suits every business. The best industrial flooring depends on the demands of your industry, the environment and your day-to-day operations.
Epoxy resin flooring remains an excellent all-round solution for manufacturing, warehousing and automotive environments. Polyurethane cement flooring excels in food production and other hygiene-critical settings. Heavy-duty resin systems and specialist chemical-resistant coatings all offer valuable benefits for specific applications.
By investing in the right industrial flooring and maintaining it correctly, businesses can improve safety, reduce long-term maintenance costs and create a more efficient working environment. If you’re unsure which flooring system is best for your facility, seek professional guidance or read our flooring guides.